


Conbit
159 Case Studies
A Conbit Case Study
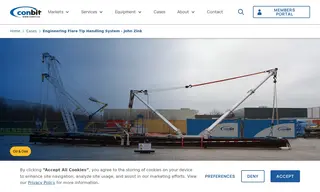
The customer, John Zink Hamworthy Combustion, the largest flare tip manufacturer, faced the challenge of replacing flare tips during a shutdown with minimal time and unknown conditions at the top of the flare tower. They awarded Conbit an engineering contract followed by a contract to supply a specialized flare tip handling system to address this.
Conbit engineered and supplied a modular mechanical handling system constructed from lightweight components, designed to be assembled on the flare tip access platform. This solution eliminated the need for pre-shutdown provisions in the heat radiated zone, guaranteeing a working system and contributing to a safer, more efficient shutdown process. The winch remained at deck level and no component exceeded 16 kgs, facilitating easier handling.
159 Case Studies